Filtration Mechanism and Media Design: Surface vs Depth Filtration
Selecting the appropriate particulate capture architecture demands a comprehensive analysis of micro-filtration physics. Baghouse and pleated cartridge dust collectors arrest airborne dust using fundamentally distinct media structures, pulse-jet cleaning dynamics, and interstitial gas velocities. DARKO Cement Machinery delivers specialized industrial filtration engineering to help operators balance stringent air quality compliance with dependable, long-term processing throughput.
Pulse-Jet Baghouse Filtration
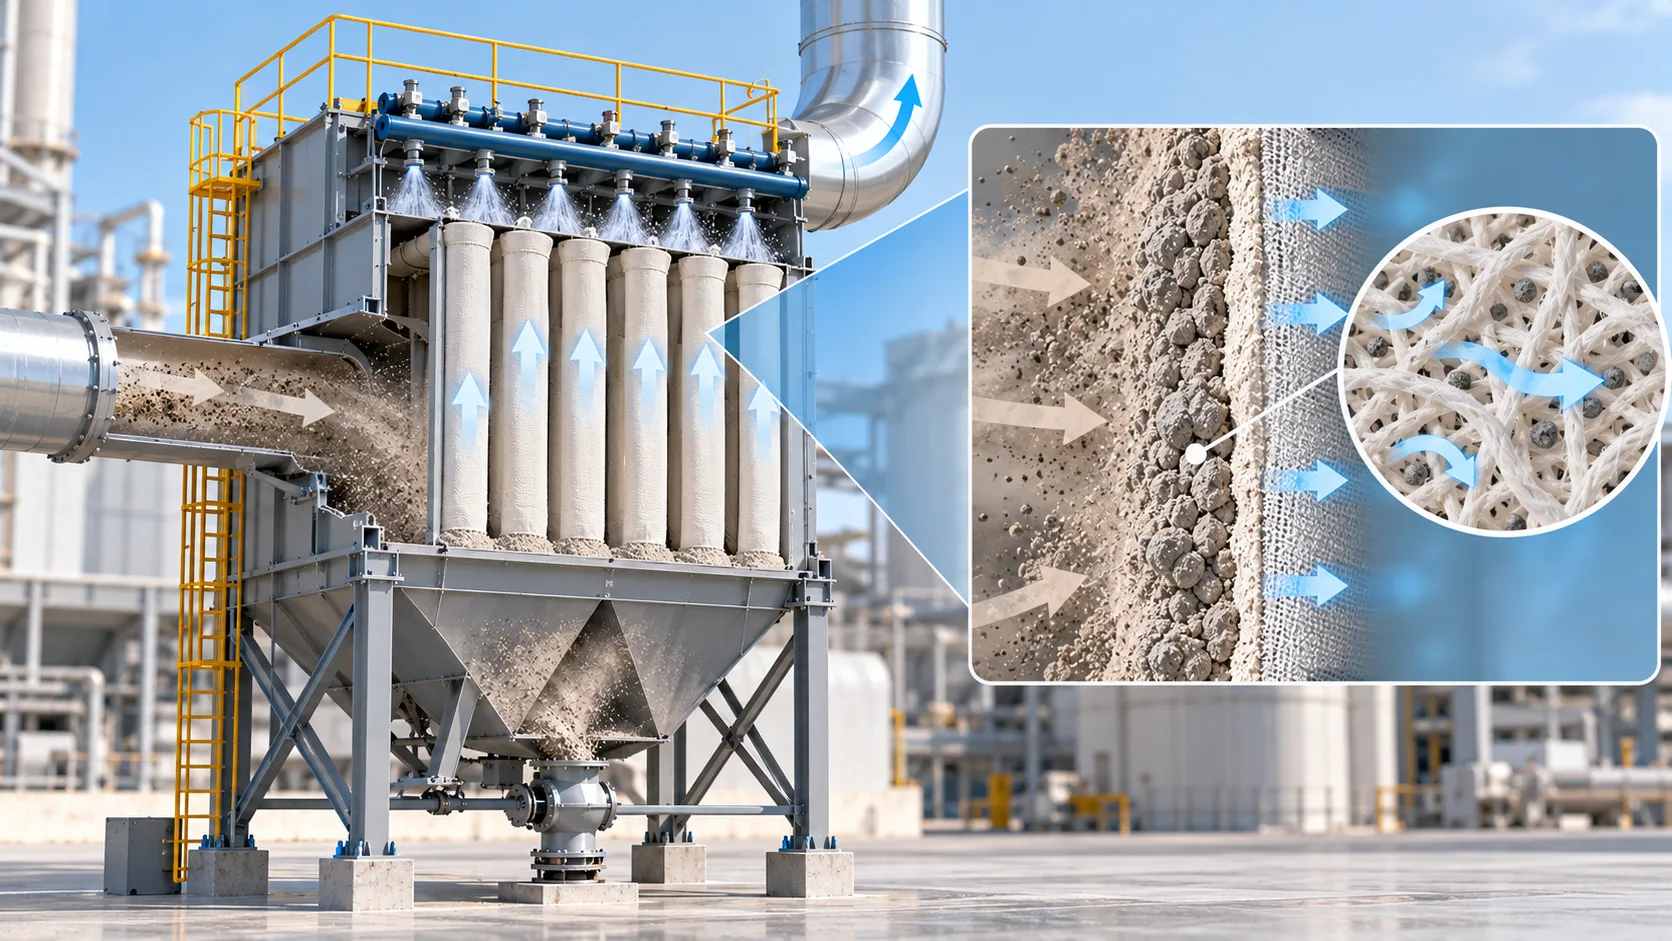
Industrial baghouse dust collectors utilize elongated cylindrical needle-felt or woven fabric bags mounted over rigid metal support cages. Particulate-laden process gas enters the housing and travels outside-in, forming a porous, permeable dust cake over the fabric exterior. This stratified dust layer serves as the primary barrier, delivering exceptionally stable depth filtration even under rigorous industrial dust loadings.
Key Engineering Characteristics
- ✓ Media Construction: Heavy-duty nonwoven needle-felt (polyester, fiberglass, PPS, PTFE membrane, or P84 polyimide) rated at 14–18 oz/yd² density.
- ✓ Dust Load Capacity: Reliably processes severe grain loadings exceeding 50 g/m³ without triggering catastrophic differential pressure spikes.
- ✓ Pulse-Jet Cleaning: High-energy reverse compressed air pulses (0.4–0.6 MPa) flex the fabric, shearing off the dust cake cleanly into the discharge hopper.
Pleated Cartridge Collector
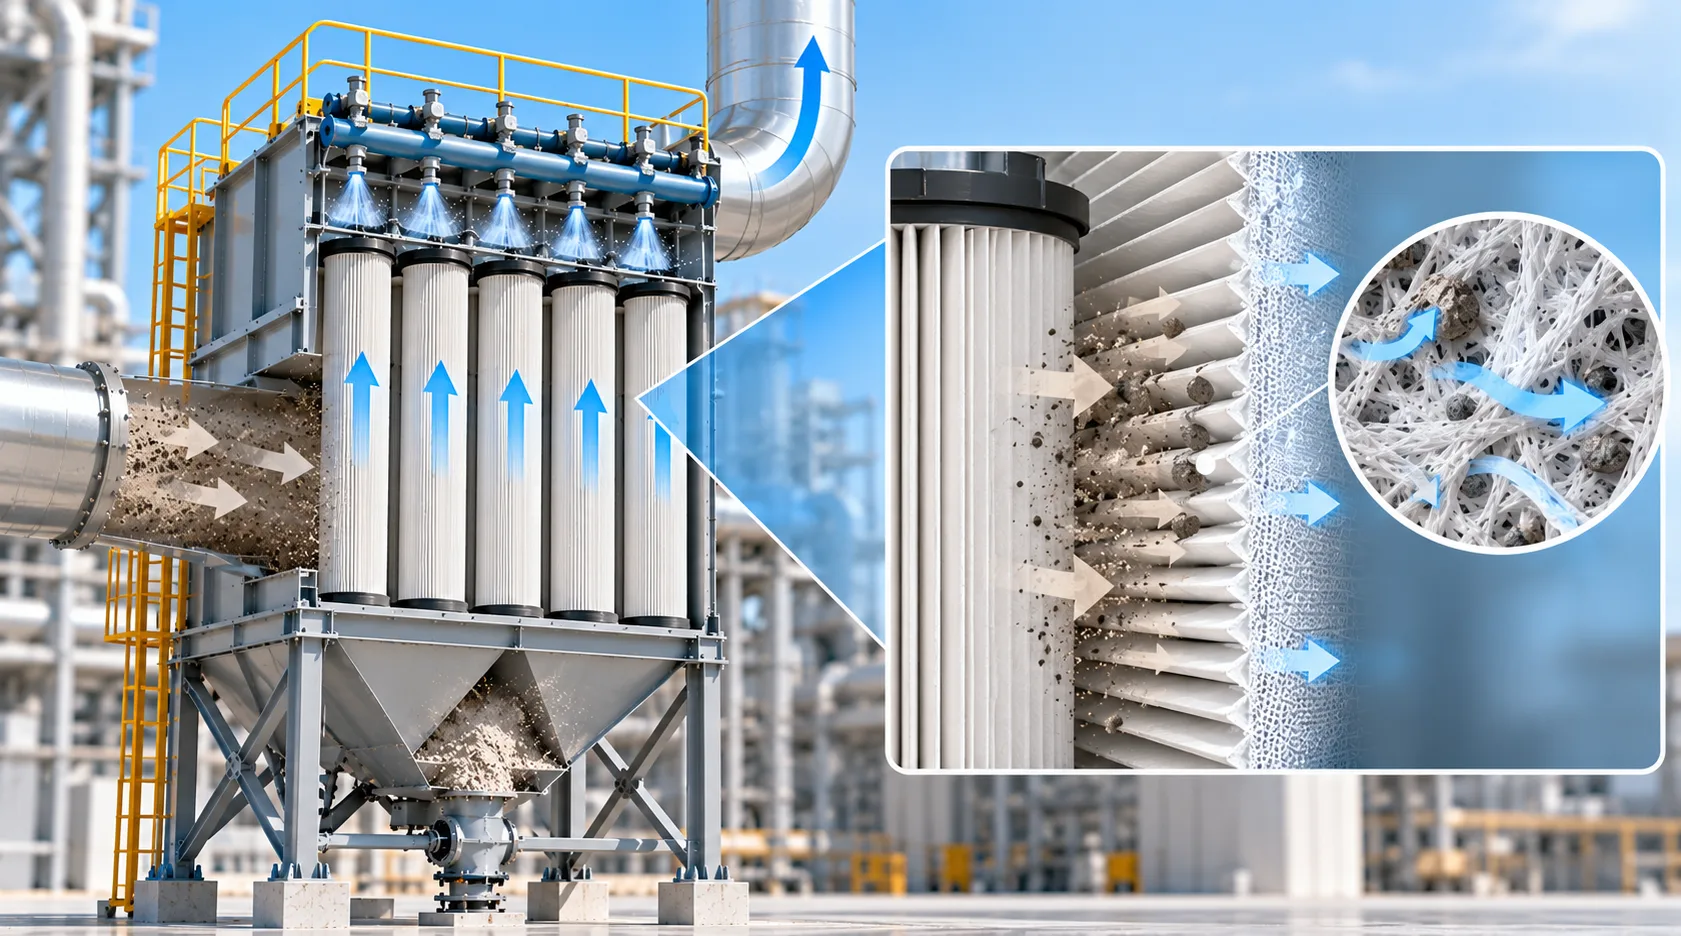
Cartridge dust collectors incorporate continuous pleated media substrates—typically spunbond polyester, cellulose blends, or advanced nanofiber webs. By folding the filter media into dense pleat geometries, these units provide extensive filtration surface area within an ultra-compact footprint, utilizing direct surface interception to capture sub-micron particulate before depth penetration occurs.
Key Engineering Characteristics
- ✓ Media Construction: Deeply pleated non-woven polyester or synthetic substrates coated with electrospun nanofibers or ePTFE surface membranes.
- ✓ Dust Load Capacity: Optimized for light to moderate dust concentrations (<15 g/m³) and free-flowing, non-agglomerating particulate streams.
- ✓ Pulse-Jet Cleaning: Low-pressure, high-volume reverse pulses calibrated to prevent pleat pinching and eliminate particulate re-entrainment.
Air-to-Cloth (A/C) Ratio Mechanics and Interstitial Velocity
The Air-to-Cloth (A/C) ratio, also expressed as filtration velocity, measures the volumetric gas flow rate (CFM or m³/min) relative to the active media area (ft² or m²). Sizing this parameter correctly is the single most critical factor in preventing premature media blinding, maintaining stable system resistance, and safeguarding long filter service life.
Wide spacing between cylindrical filter bags ensures low upward interstitial can velocity. This aerodynamic clearance permits dislodged heavy dust cakes to fall smoothly into the collection hopper during online pulse cycles without immediately re-depositing on neighboring bags.
Although pleated cartridges provide significantly more square footage per unit volume, they require conservative filtration velocities when handling fine dust. Elevated air velocity drives particulate deep into narrow pleat roots, choking media channels and rendering reverse pulsing ineffective.
Pulse-Jet Dynamics: Pressure Drop vs Media Longevity
Baghouses use high-pressure supersonic pulse waves guided by venturi nozzles to expand needle-felt bags rapidly outward, fracturing the outer dust cake cleanly along the full length of the filter.
Excessive pulse pressure or high dust loading in cartridge collectors can collapse pleat walls together, packing dust irreversibly into the inner pleat valleys and restricting overall airflow.
Leveraging precision-engineered filter bags and cages, DARKO ensures optimal gas distribution and pulse cleaning release across demanding processing systems.
Engineering Specifications Matrix: Baghouse vs Cartridge
Evaluating industrial air pollution control systems requires balancing critical thermal thresholds, dust loading capacity, spatial constraints, and long-term fan energy penalties. Plant engineers must evaluate upfront capital outlay against recurring differential pressure and media changeout costs when comparing pulse-jet baghouses and pleated cartridge collectors.
DARKO Cement Machinery designs heavy-duty baghouse dust collectors and modular cartridge systems tailored to strict particulate emission standards. The technical parameters comparison matrix below contrasts structural footprints, aerodynamic velocity limits, and filtration performance across standard ambient processes and demanding cement production environments.
Technical Parameters Comparison
Switch between operating regimes to review sizing criteria, differential pressure targets, and media limitations.
| Technical Parameter | Pulse-Jet Baghouse Collector | Pleated Cartridge Dust Collector |
|---|---|---|
| Continuous Operating Temperature | Up to 260°C (500°F) Continuous Utilizes woven fiberglass, expanded PTFE membrane, or P84 polyimide felt to handle hot, acidic process flue gases. | 65°C – 80°C (150°F – 176°F) Standard Specialty aramid media extends threshold to 135°C; structural hot-melt pleat bonding risks failure at higher thermal exposure. |
| Inlet Dust Loading Capacity | 50 g/m³ (Heavy-Duty Grain Loading) Generous inter-bag spacing supports free gravitational particulate settling directly into hoppers without particulate bridging. | < 15 g/m³ (Low to Moderate Grain Loading) Heavy particulate streams bridge tightly packed pleat roots, choking effective filtration area and causing premature blinding. |
| Collector Footprint & Overhead Clearance | Larger Footprint; Substantial Crane Headroom Demands vertical crane and monorail clearance above the tubesheet (typically 3 to 6 meters) for filter bag and cage removal. | 40% – 60% Footprint Reduction; Low Headroom High surface-area-to-volume ratio with side- or front-access clamped doors allows direct installation in height-restricted areas. |
| Design Air-to-Cloth Ratio | 1.0 : 1 to 2.5 : 1 m/min (FPM) Controlled interstitial can velocity maintains stable dust cake permeability while safeguarding fabric fibers against high-speed abrasion. | 0.5 : 1 to 1.5 : 1 m/min (FPM) Large effective filter area accommodates high total airflow; conservative ratings prevent particulate re-entrainment along pleat valleys. |
| Operating Differential Pressure | 1,000 – 1,500 Pa (4.0 – 6.0 in. w.g.) Maintains predictable, steady operating resistance across fluctuating gas temperatures and abrasive clinker dust surges. | 500 – 1,000 Pa Baseline; Susceptible to Moisture Spikes Lower clean media start-up pressure, but vulnerable to irreversible delta-P spikes when processing hygroscopic or condensable dusts. |
| Maintenance Schedule & Media Longevity | 2 to 4-Year Service Life; Higher Changeout Labor Robust fabric and cage construction withstands aggressive mechanical flex and abrasive wear, though individual element replacement takes longer. | 1 to 2-Year Service Life; Fast Element Replacement Tool-free quick-release cartridge tracks cut maintenance labor and downtime, though replacement media involves higher per-unit costs. |
Engineering Selection Rule of Thumb
High operating temperatures, abrasive clinker or raw meal, and high inlet grain loadings (>50 g/m³) mandate industrial pulse-jet baghouses. Enclosed spaces, low-to-moderate ambient dust streams, sub-micron particulate targets, and strict footprint limits strongly favor pleated cartridge dust collectors.
Mechanical Gas Dynamics in Severe Regimes
In heavy industrial environments like cement production lines, kiln exhaust streams carry abrasive calcined particulate along with elevated process moisture and acid gas compounds. Pulse-jet baghouses excel under these severe conditions because needle felt and woven fabrics encourage the formation of an initial porous dust cake. This protective layer serves as the primary filtration barrier, safeguarding underlying fibers and maintaining controlled differential pressure during high-pressure reverse pulse cleaning.
- Abrasion Resistance: Heavy cylindrical filter bags supported by structural wire cages endure high interstitial turbulence without localized media fatigue.
- Moisture Resilience: Specialized needle felts with oleophobic and PTFE surface treatments shed sticky raw meal particulate during kiln startups and temperature dips.
Aerodynamic Advantages of Pleated Cartridge Media
Pleated cartridge dust collectors consolidate large filtration surface areas into compact structural housings using pleated spunbond polyester or cellulose media. For finished cement packaging lines, telescopic loading spouts, and silo bin venting, this geometry provides maximum collection efficiency within a compact footprint, significantly reducing structural steel requirements and crane lifting overhead.
- Sub-Micron Capture: Spunbond polyester media with thermally bonded nanofiber or PTFE membranes captures fine dust down to 0.3 microns at >99.99% efficiency.
- Rapid Serviceability: Horizontal or vertical quick-release slide-out tracks enable fast cartridge changeouts directly from outside the dirty-air housing.
Engineered Gas Plenums and Heavy-Duty Fabrication
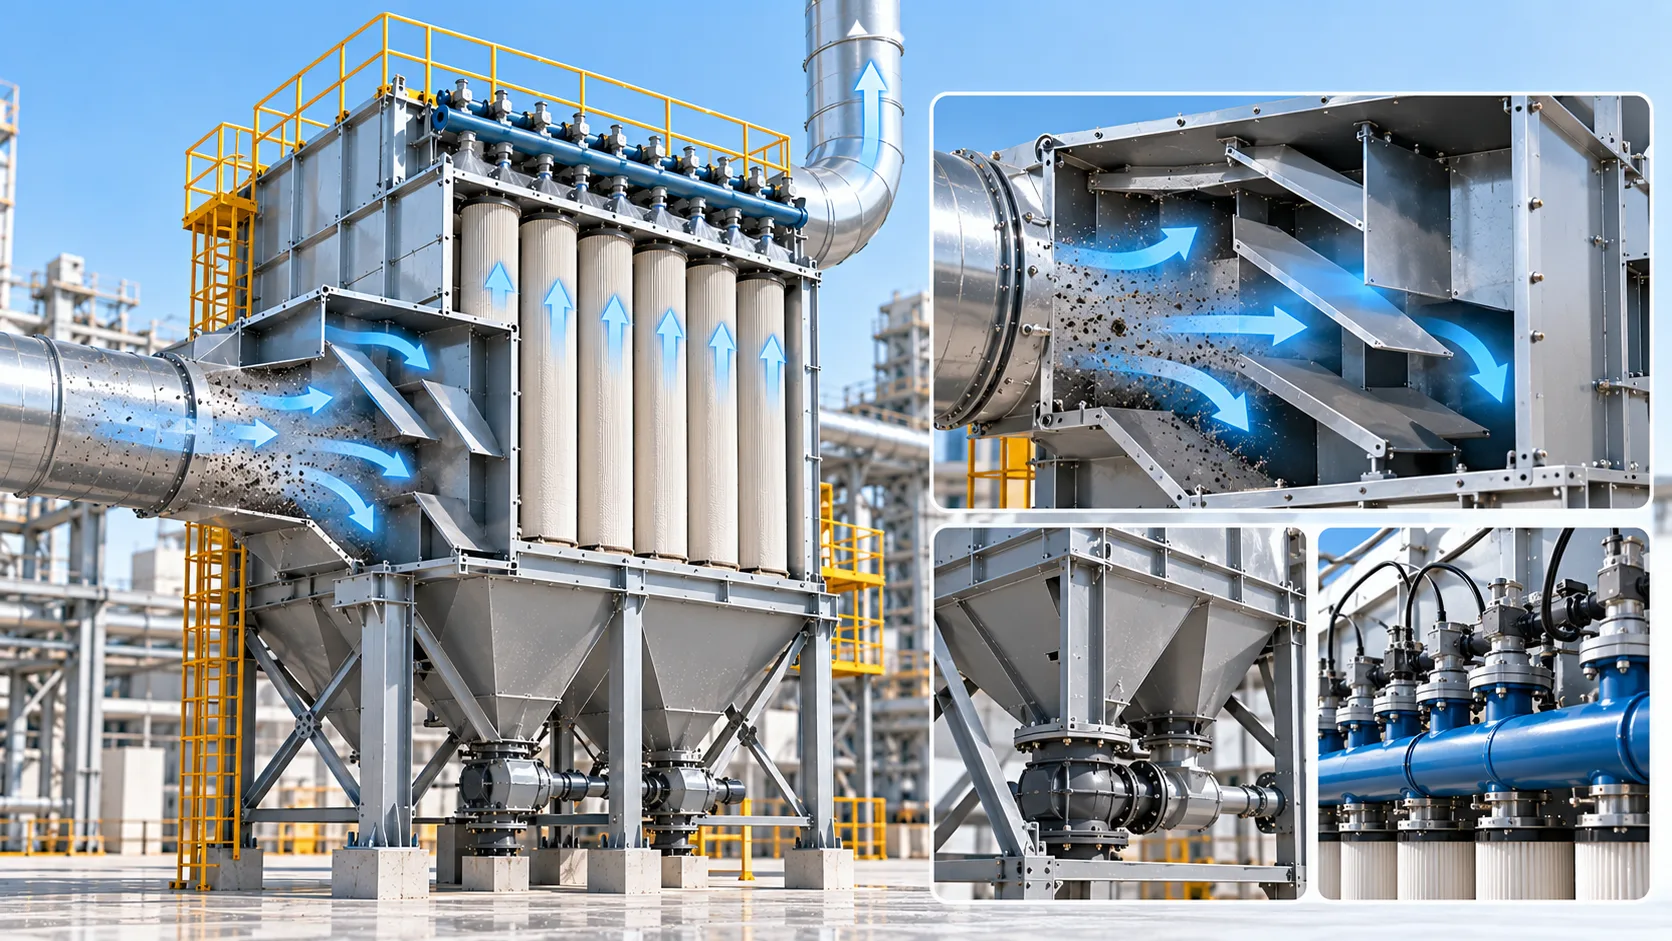
DARKO Cement Machinery fabricates industrial pulse-jet dust collectors with CFD-optimized raw gas inlet plenums, integrated drop-out baffles, and heavy-gauge hopper assemblies. Directing the incoming gas velocity prevents localized particulate abrasion on filter elements and ensures uniform air distribution across the entire bag or cartridge array.
Review detailed collector dimensions, connection flange specifications, and compressed air manifold requirements tailored to your plant layout constraints.
Industrial Application Suitability in Bulk Material Handling
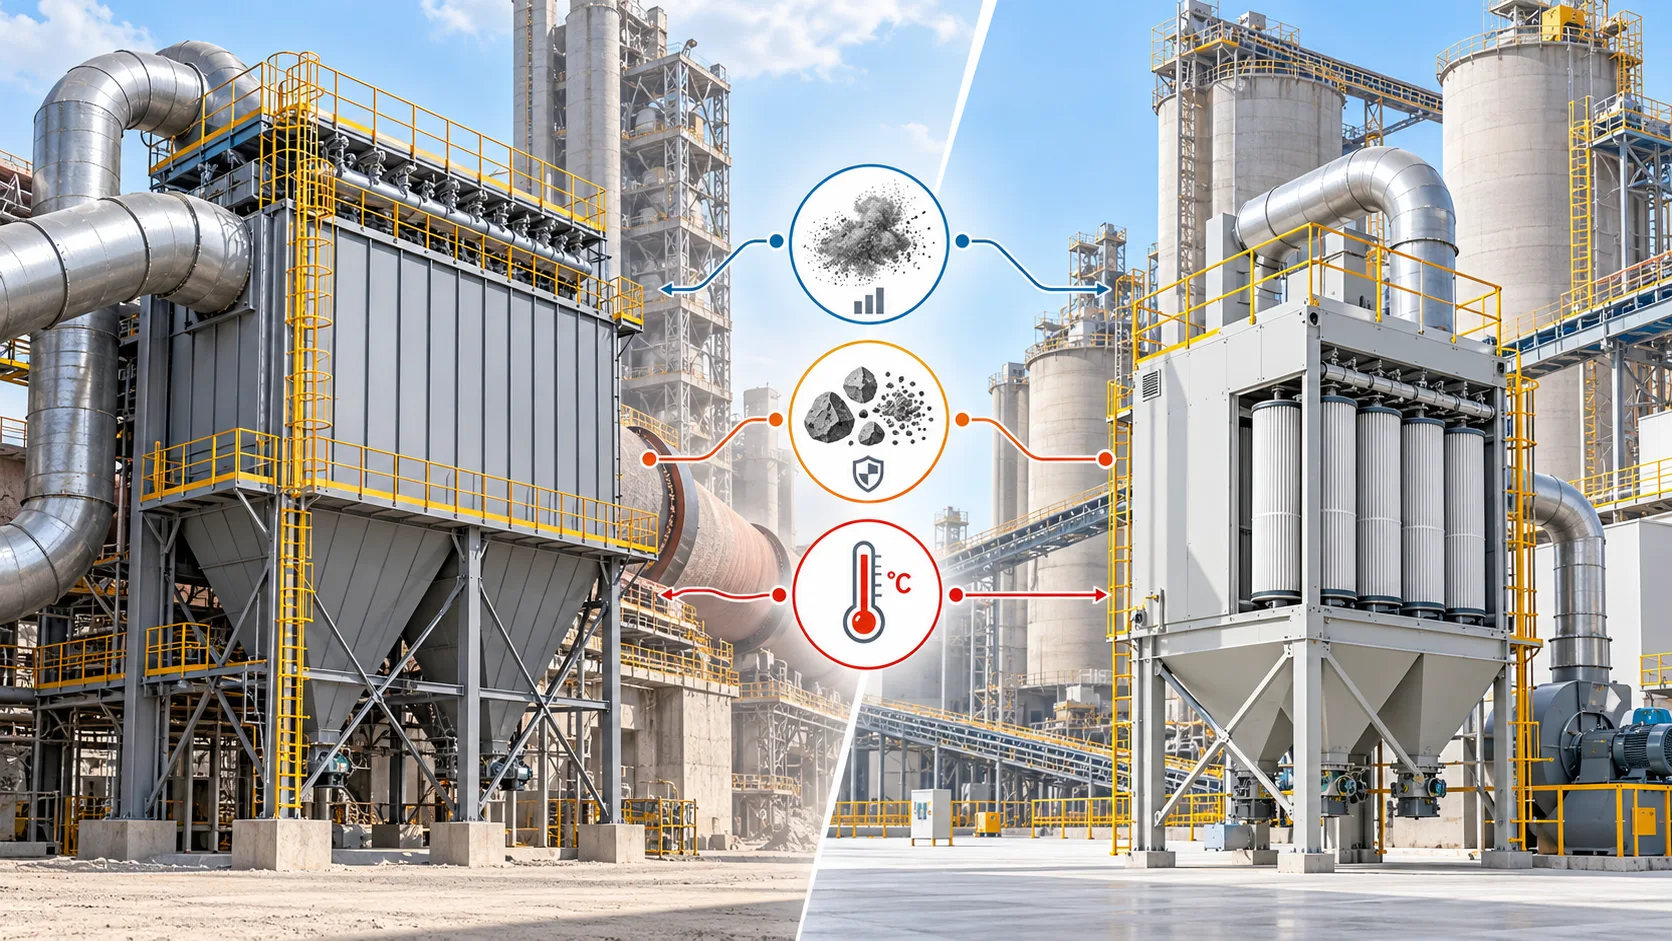
Specifying between a baghouse vs cartridge dust collector requires rigorous evaluation of process gas chemistry, grain loading, thermal excursions, and structural envelope constraints. Across integrated cement plants and heavy bulk powder terminals, equipment selection directly governs particulate emission limits and plant availability. DARKO Cement Machinery engineers heavy-duty baghouse dust collectors for pyroprocessing gas streams and compact cartridge dust collectors for localized venting, ensuring reliable emission compliance across every processing stage.
Kiln Exhaust, Raw Grinding Mills, and Clinker Coolers
High-temperature heavy dust loading environments demand rugged fabric filtration capable of continuous operation under extreme thermal stress, abrasive particle velocity, and fluctuating moisture levels.
Operating Parameters
- Operating Temperature: Continuous duty up to 260°C (500°F)
- Inlet Dust Loading: Severe grain burdens exceeding 50 g/Nm³
- Media Abrasion Profile: Highly abrasive clinker, limestone, and slag
Engineering Assessment: Pyroprocessing exhaust temperatures degrade standard cartridge bonding adhesives, while coarse clinker particulate bridges narrow pleat spacing. Heavy-duty pulse-jet baghouses utilizing woven fiberglass or PTFE-membrane felt bags provide the mechanical resilience and cake release required for uninterrupted kiln campaigns.
Telescopic Bulk Truck Loading and Silo Top Venting
Storage silo venting and mobile loading spouts demand maximum filtration surface area within an ultra-compact envelope to limit structural steel loads and eliminate external ducting runs.
Operating Parameters
- Operating Temperature: Dry ambient to moderate process heat (<65°C)
- Dust Concentration: Intermittent, low-to-medium grain loading (<15 g/Nm³)
- Installation Constraints: Restricted roof headroom and strict weight allowances
Engineering Assessment: Silo top dust filter installations capitalize on the small footprint and high media density of pleated elements. Directly mounting flanged bin vents on silo roofs avoids hopper bridging, reduces layout dead loads, and enables tool-free horizontal element servicing without overhead crane access.
Conveyor Transfers, Air Slides, and Bucket Elevators
Intermediate drop chutes and continuous mechanical transfer points present moderate dust volumes where equipment selection hinges on available mezzanine clearances and maintenance procedures.
Operating Parameters
- Operating Temperature: Non-condensing ambient conditions (20°C to 60°C)
- Dust Concentration: Continuous intermediate loading (10 to 30 g/Nm³)
- Maintenance Strategy: Multi-year bag life vs rapid cartridge changeouts
Engineering Assessment: Traditional pulse-jet baghouses excel where ample vertical height permits long cylindrical bags with extended wear cycles under continuous abrasive impact. Conversely, compact cartridge collectors are preferred when vertical overhead clearance is limited and quick side-access maintenance is prioritized.
Process Boundary Engineering Guidance
High-temperature gas flows, elevated moisture content, and aggressive dust loadings often favor appropriately engineered pulse-jet baghouse systems. Cartridge collectors are well suited to many ambient-temperature venting applications where compact installation and efficient fine-particle filtration are priorities. Explore DARKO's industrial dust collection equipment to identify a suitable configuration for your operating conditions.
Total Cost of Ownership: Initial Investment vs Long-Term Maintenance
Evaluating the true economics of industrial baghouse dust collectors versus pleated cartridge dust collectors requires looking far beyond the equipment invoice. While initial capital expenditure (CAPEX) favors smaller cartridge footprints, multi-year operating expenditure (OPEX) is dictated by media replacement intervals, compressed air consumption, and changeout downtime labor. In heavy abrasive environments such as cement milling, clinker cooling, and raw bulk handling, media durability and resistance to blinding determine the cumulative balance sheet. DARKO Cement Machinery engineers heavy-duty filtration systems that balance upfront hardware costs against long-term maintenance economics to protect your plant operating margins.
Initial Hardware Outlay
Cartridge collectors reduce upfront capital cost by 15% to 30% for equivalent design airflows. Their compact modular structure cuts required steel tonnage, foundation concrete, crane mobilization, and site delivery volume.
Filter Replacement Cycle
Heavy-duty needle felt and woven filter bags achieve operating lifespans of 2 to 4 years under abrasive dust loads. Pleated cartridges typically require replacement every 1 to 2 years at significantly higher unit media costs.
Compressed Air Demand
Cartridge pleat roots trap fine particulates, requiring frequent pulse-jet cycles that increase air compressor load. Baghouses rely on uniform surface cake release, running on lower pulse frequencies with reduced air volume.
Changeout Turnaround
Side-access doors and toolless cartridge clamps allow fast element replacement without confined space entry. Baghouse cage removal and snap-band bag reinstallation require more labor hours during scheduled plant outages.
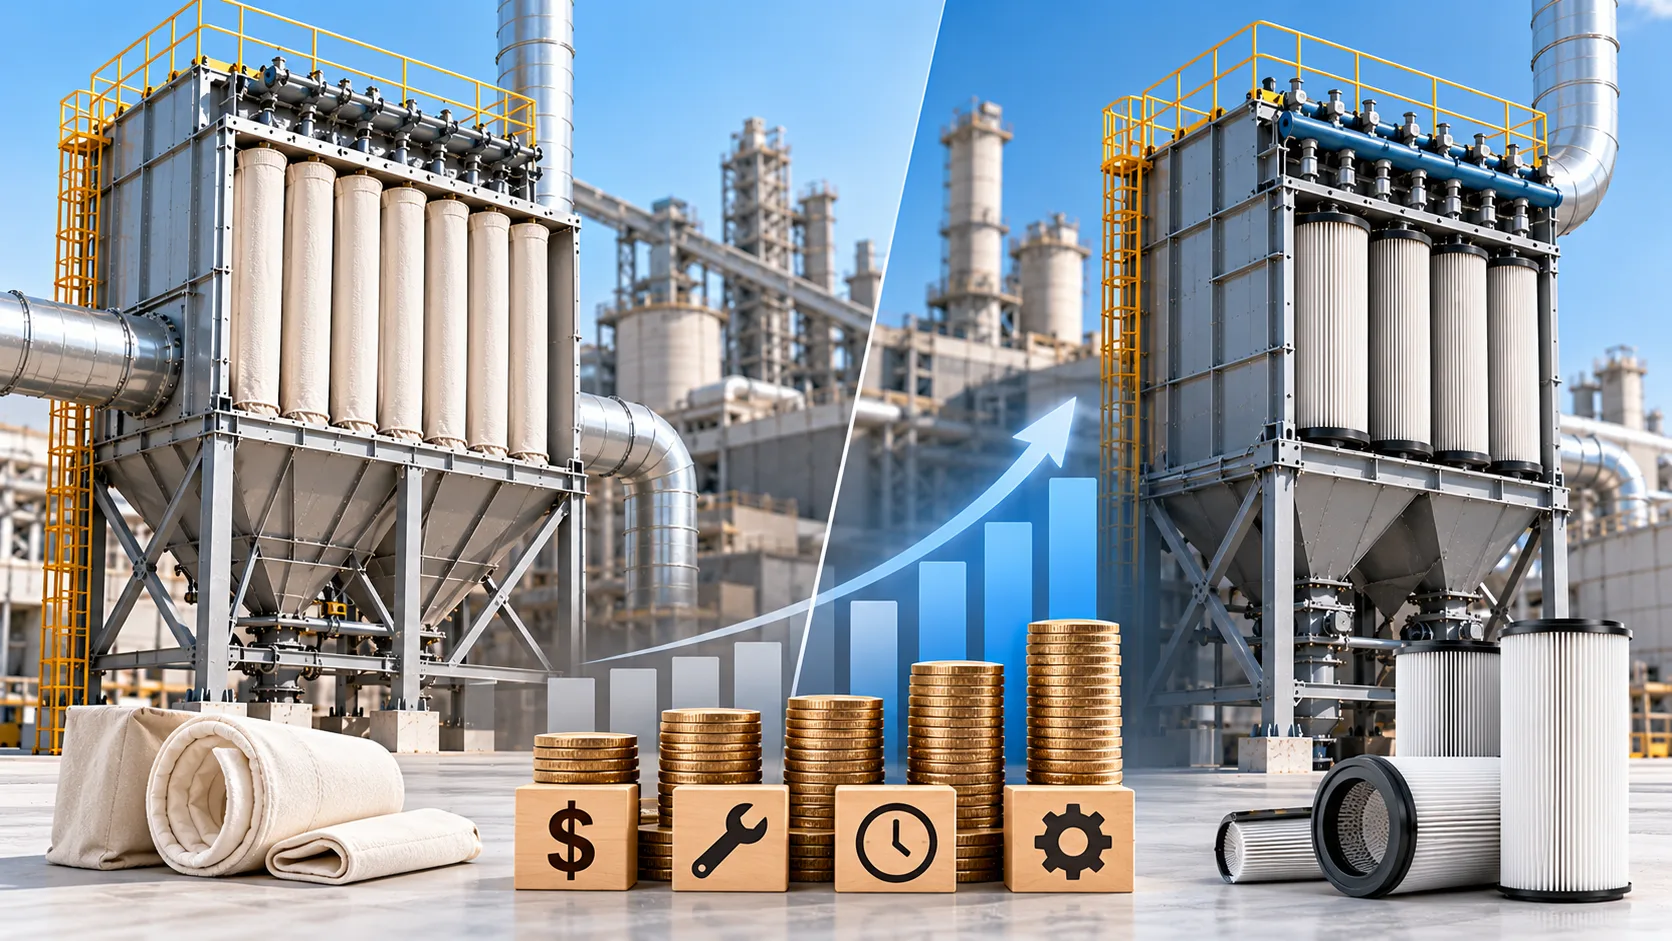
Pulse-Jet Baghouse Economic Profile
Heavy-Duty & High VolumeFabric filter baghouses demand higher structural steel mass, larger hopper footprints, and overhead crane clearances during initial plant construction. However, when operating under heavy dust concentrations (>50 g/m³), high exhaust gas temperatures (>150°C), or abrasive minerals, the robust construction of baghouse systems delivers exceptional operating cost stability over multi-year production campaigns.
Standard polyester, woven fiberglass, and PTFE needle felt sleeves remain cost-effective consumables produced by established industrial textile supply chains worldwide.
Uniform dust cake release requires fewer pulse intervals, decreasing plant compressed air demand and reducing continuous electrical load on compressor packages.
A thick, porous dust cake buffers the underlying fabric against sudden moisture spikes and grain surges, preventing premature filter blinding and catastrophic pressure drops.
Economic Takeaway: Baghouses deliver lower total cost of ownership when continuous annual runtime exceeds 6,500 hours under heavy dust loading, high temperatures, or abrasive clinker processing.
Pleated Cartridge Collector Economic Profile
Compact & Modular OutlayCartridge dust collectors significantly reduce casing dimensions, support steel tonnage, and foundation load requirements. This compact footprint lowers initial turnkey capital expenditure and accelerates field erection schedules, making cartridge units an attractive economic choice for bin vents, truck loadout spouts, conveyor transfers, and indoor grinding circuits.
Saving 40% to 60% in physical footprint avoids costly building expansions, reduces mezzanine steel requirements, and minimizes dead weight on silo top decks.
Front-opening access hatches and tool-free clamping mechanisms allow a two-person maintenance crew to replace all cartridge elements in a single work shift.
Pleated construction with thermally bonded end caps, internal mesh cores, and ePTFE membrane treatments results in higher replacement costs per square meter of filter area.
Economic Takeaway: Cartridge systems offer superior economic return on moderate dust concentrations (<15 g/m³) and ambient temperature streams where space constraints govern installation feasibility.
Five-Year Cumulative Cost Horizon Analysis
Lifecycle cost model combining initial procurement, replacement media, compressed air utilities, and maintenance labor.
Normalized indices reflect a typical 15,000 CFM industrial ventilation installation operating 8,000 hours per year under standard industrial electric utility rates, factoring in pulse valve rebuilds, consumable filter replacements, and scheduled downtime labor.
Critical Wear Item Registry & Inspection Protocols
Component reliability profiles, planned service intervals, and primary failure mechanisms under continuous heavy industrial plant duty.
| System Component | Collector Configuration | Service Life Expectancy | Primary Failure Mechanism | Economic Impact of Neglect |
|---|---|---|---|---|
| Needle Felt Filter Bags | Pulse-Jet Baghouse | 24 to 48 Months | Abrasive fiber thinning, localized cage rub, thermal-mechanical fatigue | Particulate emissions limit breaches, stack opacity penalties, duct sanding |
| Pleated Filter Elements | Cartridge Collector | 12 to 24 Months | Pleat root dust compaction, interstitial bridging, end-cap potting breakdown | Steep differential pressure spikes, fan motor overload, reduced capture velocity |
| Internal Wire Support Cages | Pulse-Jet Baghouse | 60 to 96 Months | Acid-gas pitting corrosion, weld separation, longitudinal structural buckling | Accelerated bag cuts, collapsed filter sleeves, blocked internal gas passages |
| Diaphragm Pulse Valves | Dual Configuration | 1,000,000 Pulse Cycles | Elastomer diaphragm hardening, return spring fatigue, pilot solenoid wear | Continuous compressed air leaks, weakened cleaning pulse, accelerated media cake build |
| Venturi Induction Nozzles | Pulse-Jet Baghouse | 72 to 120 Months | Erosive throat wall thinning from entrained abrasive raw particulates | Diminished secondary pulse air entrainment, reduced cleaning efficiency |
Through heavy-gauge casing fabrication, precision-engineered venturi nozzles, and durable OEM filter cages and bags, DARKO Cement Machinery systems minimize unplanned maintenance downtime across demanding multi-year operating campaigns. Our applications engineering team conducts comprehensive lifecycle cost analyses to guide your facility toward the most cost-effective dust collection architecture before capital commitment.
5-Step Engineering Selection Roadmap
DARKO Cement Machinery applies a structured, data-driven workflow across our dust collection equipment to determine whether a pulse-jet baghouse or cartridge collector delivers optimal performance and compliance.
Characterize Process Airflow
Quantify total volumetric flow, operating temperatures, moisture levels, and acid dew point thresholds.
- ✓ Total Airflow (m³/h or CFM)
- ✓ Continuous & Peak Temp (°C)
- ✓ Relative Humidity & Moisture %
Analyze Dust Mechanics
Evaluate inlet grain loading, particle distribution, abrasiveness, and moisture-induced caking tendencies.
- ✓ Grain Loading (g/m³ or gr/dscf)
- ✓ Abrasiveness & Particle Size
- ✓ Hygroscopic & Kst Explosivity
Audit Spatial Constraints
Inspect available installation footprint, overhead clearance for cage removal, and structural load ratings.
- ✓ Overhead Pull-Out Clearance
- ✓ Footprint & Hopper Angles
- ✓ Structural Weight Capacities
Calculate Safe A/C Ratio
Apply conservative filtration velocity parameters to define total required net and gross media surface area.
- ✓ Media Fabric Selection (e.g. PTFE)
- ✓ Interstitial Can Velocity Limits
- ✓ Total Cloth Area Calculation (m²)
Size Utilities & Emissions
Specify pulse-jet cleaning air volume, verify compressed air capacity, and validate stack emission limits.
- ✓ Compressed Air Demand (Nm³/min)
- ✓ Guaranteed Stack Limits <10 mg/Nm³
- ✓ ID Fan Static Pressure Sizing
Application-Specific Selection Architecture
Selecting between pulse-jet baghouses and cartridge systems requires precise alignment with dust volume, grain abrasiveness, and thermal stress. DARKO engineers configure purpose-built filtration systems ensuring continuous regulatory compliance across raw grinding, kiln exhaust, and silo handling circuits.
Frequently Asked Questions: Baghouse vs Cartridge Filtration
Key engineering resolutions and technical comparisons for plant managers selecting industrial dust collection equipment across demanding heavy industrial operations.
Filtration Decision Support
Selecting between industrial pulse-jet dust collection systems requires a clear balance of dust loading characteristics, operating temperatures, and structural footprints.
DARKO Cement Machinery engineers routinely analyze dust sampling data to resolve chronic blinding and high differential pressure challenges in existing cement plants.
Cement raw grinding mills and pyroprocessing kiln exhausts generate extreme particulate grain loading that routinely exceeds 50 g/m³ to 100 g/m³, combined with exhaust gas temperatures reaching 180°C to 260°C. Cartridge collectors rely on closely spaced pleat matrices that become quickly bridged under heavy dust concentrations.
Additionally, traces of acid moisture and chemical dew points create sticky agglomerations inside deep pleat roots. This leads to irreversible media blinding, pulse cleaning failure, and severe differential pressure spikes. Heavy-duty baghouse dust collectors utilizing cylindrical needle felt or woven fiberglass bags remain the standard design for harsh cement processing lines.
Yes. When properly applied in dry, light-to-moderate dust streams under 15 g/m³, advanced pleated cartridge media equipped with ePTFE membranes or spunbond nanofiber layers excel at capturing sub-micron PM2.5 particulates.
- Ultra-Clean Output: Emits below 5 mg/Nm³ under regulated dry airflow velocities.
- Surface Filtration: The membrane layer stops fine particles right at the surface, preventing deep pore penetration.
- Pulse Cleanability: Standard reverse pulse pulses remove surface dust cakes efficiently at conservative air-to-cloth ratios.
For dry bulk materials handling, silo venting, and railcar loadout stations, modern cartridge dust collectors easily match or surpass traditional baghouse clean-air emission standards.
Pulse-jet baghouses handle hygroscopic, moisture-laden, or condensable gas streams significantly better than cartridge units. The narrow geometry of pleat valleys makes cartridge units vulnerable to permanent mudding when moisture mixes with fine mineral dusts.
Conversely, baghouses can be equipped with oleophobic and hydrophobic treated needle felts, PTFE membrane laminates, or auxiliary lime pre-coating systems. The mechanical flexing of vertical filter bags during high-pressure pulse cycles reliably dislodges semi-adherent cakes, preventing premature media blinding.
Retrofitting standard cylindrical bags and cages with molded pleated filter bags is an effective strategy when plant expansion demands a 30% to 50% increase in airflow capacity without expanding the physical collector footprint.
Installs directly into existing tube sheets; substantially lowers system operating differential pressure; reduces can velocity.
Restricted to gas streams below 135°C with moderate grain loads; requires clean pulse-jet header alignment.
DARKO engineering teams regularly evaluate existing fan curves, tube sheet hole configurations, and dust abrasiveness before executing pleated bag conversions.
Build a More Reliable
Dust Collection System.
Comparing baghouse and cartridge dust collectors for your facility? Share your airflow, temperature, and dust characteristics. DARKO's team can help assess filtration requirements and recommend equipment configurations for your operating conditions.
Equipment Selection
Baghouse or cartridge suitability
Application Review
Airflow, dust loading and temperature
Retrofit Consultation
Existing collector upgrade options
Spare Parts Support
Filter bags, cartridges and cages
Request Engineering Support
Tell us what you need. The technical details can be discussed after your inquiry.
Prefer direct contact? Visit Contact Us